Search Products
Automation-Induced Static: Why Modern Fabs Need to Worry More About Machines Than People
Description
Introduction
Ask an ESD engineer about the biggest source of static electricity twenty years ago, and the answer would almost certainly have been operators.
People walking across a floor, handling components without proper grounding, or working at non-compliant workstations were responsible for a large percentage of ESD incidents.
Walk into a modern semiconductor fab today and the situation looks completely different.
Operators rarely touch product. Wafers move automatically through the facility. Material transport is handled by overhead systems. Robots load process tools. Automated handlers perform inspection, testing and packaging operations.
In many advanced facilities, wafers travel hundreds of metres through the manufacturing line without direct human contact.
This has changed the nature of ESD risk.
Human Body Model (HBM) events have reduced significantly in well-controlled fabs. The bigger concern today is machine-generated charging leading to Charged Device Model (CDM) events and Charged Board Events (CBE).
The challenge is that these events are often faster, harder to detect and more damaging than traditional HBM failures.
Why HBM Is No Longer the Main Concern
Most ESD programmes were originally developed around Human Body Model protection.
The logic was straightforward.
A person accumulates charge, touches a device and the stored energy discharges into the component.
For years, this represented the dominant ESD failure mechanism in electronics manufacturing.
Modern semiconductor facilities have largely addressed this risk through:
· Continuous personnel grounding
· Conductive flooring systems
· ESD footwear
· Wrist straps
· Compliance monitoring
· Controlled workstations
As a result, genuine HBM failures have become relatively uncommon inside well-managed fabs.
Unfortunately, eliminating one problem has not eliminated ESD risk.
The source of charging has simply shifted from people to machines.
The Rise of CDM in Advanced Manufacturing
Charged Device Model events occur when the device itself becomes charged and subsequently discharges to a grounded surface.
Unlike HBM events, CDM discharges are extremely fast.
Peak current levels can be surprisingly high even when the actual voltage involved appears modest.
This is one reason why modern semiconductor devices frequently exhibit lower CDM withstand levels than HBM ratings.
A component that survives an HBM event may still fail during a CDM discharge.
As device dimensions shrink and package densities increase, CDM has become one of the most significant ESD concerns in semiconductor manufacturing.
Machines Generate More Static Than Most People Realise
There is a common assumption that automated systems are naturally safer because they eliminate human interaction.
From an ESD perspective, this is not always true.
Automation introduces numerous opportunities for charge generation.
Examples include:
· High-speed robotic motion
· Belt-driven transport systems
· Vacuum pick-up mechanisms
· Polymer contact surfaces
· Wafer handling equipment
· Packaging systems
· Automated inspection tools
Whenever two materials repeatedly contact and separate, charge generation can occur.
The basic triboelectric effect does not care whether the movement comes from a person or a machine.
In fact, machines often perform these actions thousands of times per hour, making them highly efficient static generators.
High-Speed Pick-and-Place Systems
Pick-and-place equipment represents one of the most common charging sources in electronics manufacturing.
Modern machines operate at remarkable speeds.
Components are picked, moved and placed within milliseconds.
During this process:
· Vacuum nozzles repeatedly contact devices.
· Components slide against feeder mechanisms.
· Carriers move at high speed.
· Plastic and metallic surfaces interact continuously.
Each interaction creates an opportunity for charge generation.
Most events are too small to notice individually.
However, over millions of cycles, charge accumulation can become significant.
In many investigations of unexplained yield loss, charging associated with automated handling equipment is eventually identified as a contributing factor.
AMHS: The Invisible ESD Challenge
Automated Material Handling Systems (AMHS) have become standard infrastructure in advanced semiconductor fabs.
These systems transport wafer carriers between process tools without operator involvement.
From a productivity perspective, AMHS technology is indispensable.
From an ESD perspective, it introduces unique challenges.
An AMHS network may contain:
· Polymer wheels
· Rollers
· Tracks
· Carriers
· Mechanical interfaces
· High-speed transport mechanisms
Every movement creates opportunities for triboelectric charging.
Because the transport process is continuous, charging can occur throughout the production cycle.
Without proper control measures, electrostatic potentials can develop long before a wafer reaches the next process step.
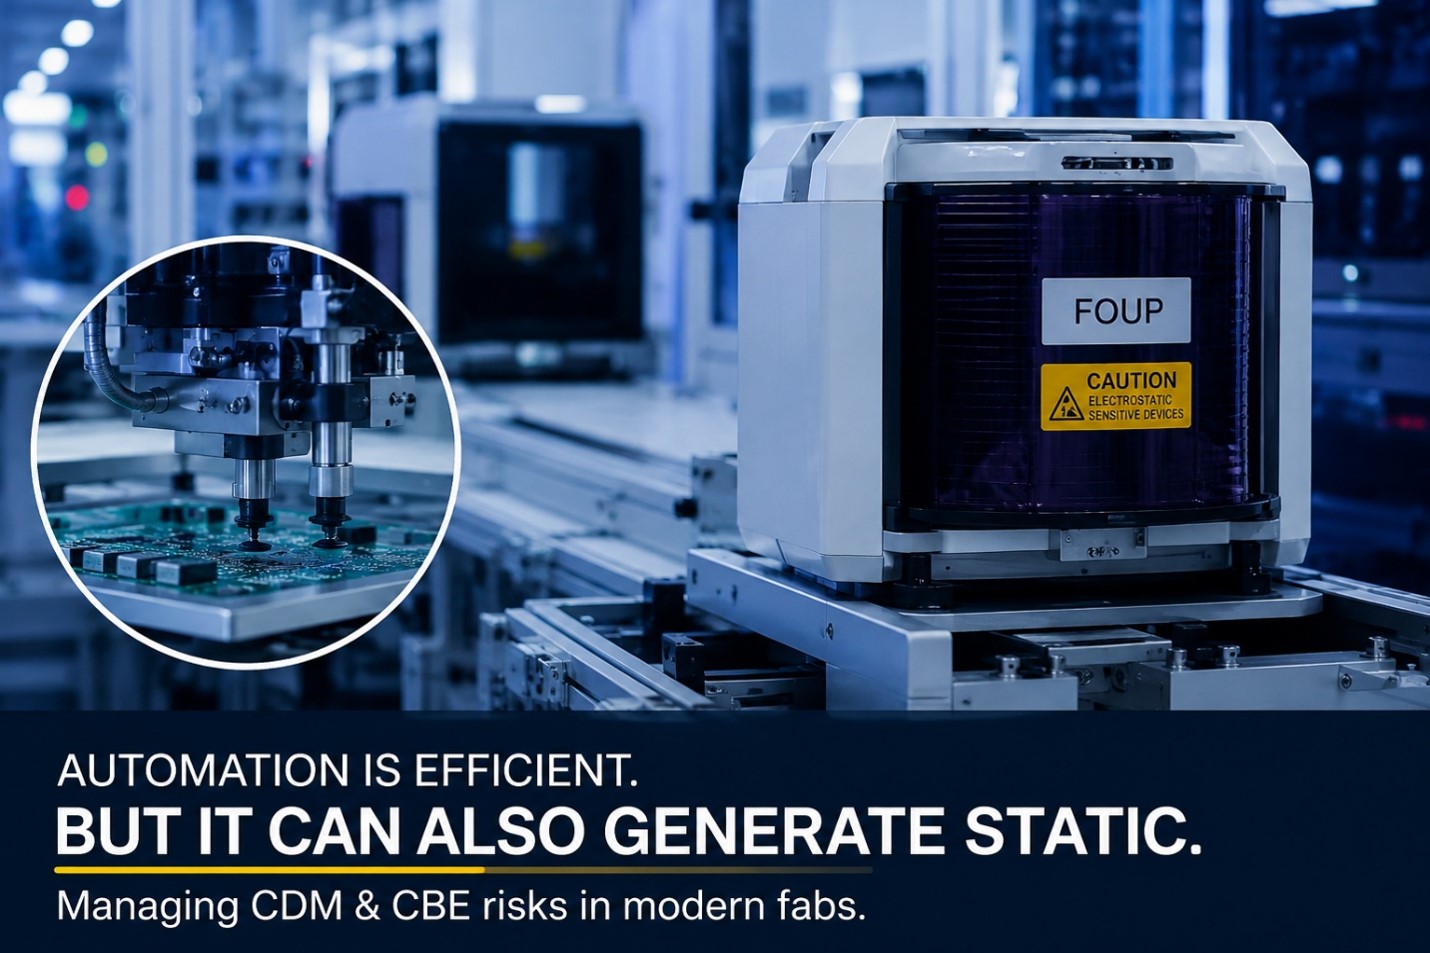
The FOUP Challenge
Few components are as critical to semiconductor manufacturing as the Front Opening Unified Pod, commonly known as the FOUP.
The FOUP protects wafers from contamination while transporting them between tools.
Most engineers immediately think about particle control when discussing FOUP performance.
However, electrostatic behaviour is equally important.
The outer shell of a FOUP is typically manufactured from specialised polymer materials.
While these materials are selected for cleanliness and mechanical performance, they can also accumulate electrostatic charge under certain operating conditions.
Sources of charging include:
· Transport movement
· Contact with automation systems
· Friction during loading and unloading
· Airflow within transport environments
· Interaction with handling equipment
The concern is not only the charge on the FOUP itself.
The concern is what happens to the wafers inside.
How a Charged FOUP Affects Wafers
A charged FOUP does not necessarily need to discharge directly into a wafer to create problems.
Electrostatic fields generated by the FOUP can induce voltages on nearby wafer surfaces.
This phenomenon becomes increasingly important as device geometries continue to shrink.
A charged polymer enclosure effectively behaves like a large capacitor surrounding the product.
Depending on the magnitude of the charge and the geometry involved, significant induced potentials can develop.
Under certain conditions, these induced voltages can contribute to CDM-type events during subsequent handling operations.
The root cause may have occurred several process steps earlier, making troubleshooting particularly difficult.
Why ESD-Safe Polymers Matter
Not all polymers behave the same way.
Traditional plastics can accumulate substantial electrostatic charge.
ESD-safe polymers are specifically engineered to control charge generation and dissipation.
Depending on the application, these materials may incorporate:
· Conductive additives
· Dissipative compounds
· Carbon-based technologies
· Specialised polymer formulations
The objective is not necessarily to make the material conductive.
Rather, the goal is to prevent excessive charge accumulation while maintaining contamination-control requirements.
For FOUPs and automated handling systems, material selection plays a major role in reducing long-term ESD risk.
Specialised Ionisation for Automated Transport
Grounding works extremely well for conductive objects.
Unfortunately, many automated handling components are made from non-conductive materials.
This is where ionisation becomes essential.
Traditional ioniser installations often focus on manual workstations and assembly areas.
Modern fabs increasingly require ionisation strategies designed specifically for automation environments.
Examples include:
· FOUP loading stations
· Stocker interfaces
· AMHS transfer points
· Robotic handling zones
· Inspection systems
· Tool load ports
The objective is to neutralise charge before it accumulates to problematic levels.
This requires careful placement, regular verification and periodic performance testing.
Simply installing an ioniser is not enough.
Its effectiveness must be confirmed under actual operating conditions.
Auditing Automation-Induced ESD Risks
One of the most interesting findings during ESD audits is how frequently charging sources are hidden inside otherwise well-controlled facilities.
Personnel grounding programmes may be excellent.
Workstations may be fully compliant.
Flooring systems may pass every test.
Yet significant charging can still occur inside automated equipment.
A thorough audit should therefore include:
· Electrostatic field measurements around automation systems.
· FOUP surface voltage assessments.
· Ionisation performance verification.
· Isolated conductor surveys.
· AMHS charging evaluations.
· Process-specific CDM risk assessments.
The objective is to understand how charge moves through the manufacturing process, not merely how individual components perform in isolation.
Conclusion
The semiconductor industry’s transition towards highly automated manufacturing has fundamentally changed the nature of ESD risk.
Today, operators are often the least significant source of charging inside a modern fab. The greater challenge lies in understanding how automated handling systems, robotic equipment, transport mechanisms and polymer-based carriers generate and transfer electrostatic charge.
As device sensitivity continues to decrease, Charged Device Model and Charged Board Events are becoming increasingly important contributors to yield loss and reliability concerns.
For ESD professionals, the question is no longer whether automation generates static electricity. It certainly does.
The real question is whether that charging is being measured, controlled and managed before it affects production yield.
In advanced manufacturing, the most dangerous ESD source is often the one moving product efficiently through the factory while nobody is looking at it.